Phone:
(701)814-6992
Physical address:
6296 Donnelly Plaza
Ratkeville, Bahamas.

Phone:
(701)814-6992
Physical address:
6296 Donnelly Plaza
Ratkeville, Bahamas.
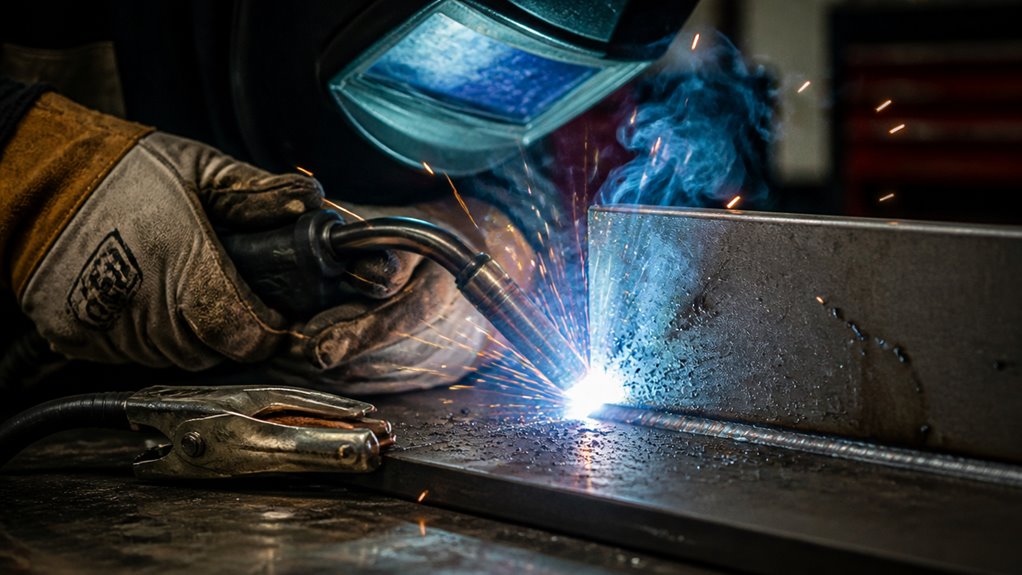
You can weld 1/4-inch steel with a 110V MIG welder, but you’ll need a high-end machine near 140 amps. Precise joint prep and multi-pass techniques are essential for adequate penetration.
Using flux-core wire helps optimize heat transfer and fusion despite voltage limits. Manage your duty cycle carefully to prevent overheating and reduce weak welds.
However, for consistent, deeper penetration and longer welds, 220V equipment is preferred. Explore machine settings and wire choices to improve your weld quality.
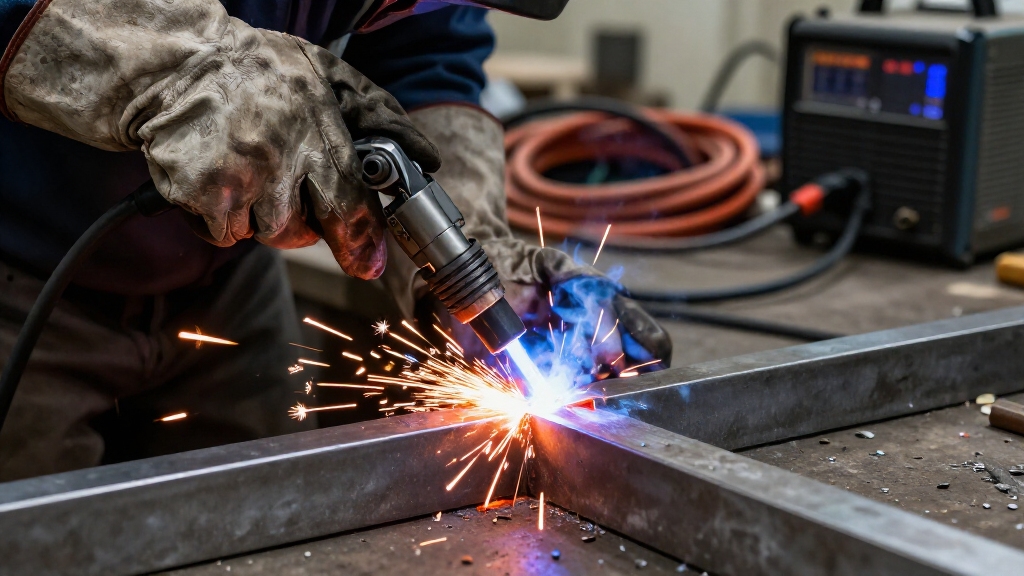
Welding 1/4-inch steel with a 110V MIG welder is possible, but it demands careful attention to machine capability and technique.
Your success hinges on using a high-end 110V machine, ideally rated near 140 amps, paired with meticulous joint preparation.
You’ll need to bevel the edges and perform multiple passes, starting with a root pass followed by fills, to achieve adequate penetration.
Single-pass welds on this thickness often yield marginal fusion and weak joints.
Maintaining a clean surface and tight fit-up is critical, as is adjusting wire speed and voltage precisely.
Due to limited duty cycles at maximum output, you must allow cooling intervals to avoid overheating.
While 110V MIGs can handle occasional 1/4-inch repairs, consistent quality demands more robust equipment and refined technique.
Proper joint prep, including beveling and surface cleaning, enhances weld quality and reduces the number of passes required.
You’ll quickly notice that 110V MIG welders struggle with 1/4-inch steel primarily due to limited amperage and heat output.
Most 110V machines deliver between 30 and 140 amps, with penetration at 1/4-inch thickness often marginal even at the upper end.
This amperage limitation restricts your ability to achieve proper fusion in a single pass, especially since the duty cycle at maximum output is low, causing overheating risks.
Additionally, the voltage alone doesn’t guarantee capability; machine design and wire type affect performance.
With 1/4-inch steel, you face challenges like inadequate heat concentration and insufficient molten pool size, which increase the likelihood of weak welds.
Consequently, 110V setups often require methodical adjustments and aren’t ideal for consistent, single-pass welding on thicker material.
It’s also important to understand machine derating on 120V, which significantly limits maximum amperage and welding capacity.
Preparing the joint properly and employing multi-pass welding techniques markedly enhance the quality of welds on 1/4-inch steel with a 110V MIG machine.
Proper joint preparation and multi-pass welding significantly improve 1/4-inch steel welds with a 110V MIG.
You need to bevel the edges to create a groove that allows adequate penetration, compensating for limited amperage.
Ensuring clean, oxide-free surfaces and tight fit-up minimizes contamination and gaps, which can weaken the weld.
Start with a root pass to establish fusion at the joint base, followed by multiple fill passes to build up the weld without overheating the metal or machine.
Each pass improves fusion and reduces the risk of incomplete penetration, critical given the 110V welder’s marginal power.
You should also control wire feed speed and voltage precisely to maintain a stable arc.
This preparation and multi-pass approach markedly improves strength and consistency on 1/4-inch steel.
Additionally, applying evenly spaced 1/4-inch tack welds helps control heat and prevent distortion during welding, ensuring a strong joint heat management techniques.
When you’re welding 1/4-inch steel using a 110V MIG, you’ll find that using flux-core wire really makes a difference. It enhances penetration compared to solid wire, which means you get a stronger fusion. That’s a big plus, right?
Plus, it helps cut down on common weld defects like porosity and slag inclusion. This improvement really boosts the overall weld quality, especially when working with thicker materials. So, if you’re tackling heavier steel, flux-core wire makes the process a lot more manageable, even with the power limitations of a 110V machine. Pretty handy, don’t you think?
Additionally, flux-core wire generates shielding gas internally, allowing for effective welding in challenging conditions without the need for external gas supply, which is ideal for outdoor and thicker materials.
Boosting penetration on 1/4-inch steel with a 110V MIG welder becomes more achievable by using flux-core wire instead of solid wire.
Flux-core wire generates a more concentrated arc and produces its own shielding gas through flux decomposition. This enhances arc stability and heat concentration.
This increased thermal energy allows deeper fusion into thicker steel sections than solid wire paired with external shielding gas. Additionally, the slag created by flux-core wire slows cooling, promoting better metallurgical bonding and improved penetration depth.
While your 110V machine’s amperage limits penetration inherently, flux-core wire maximizes heat transfer efficiency within those constraints. Consequently, you gain a more robust weld bead on 1/4-inch steel, improving joint strength without upgrading to a higher-voltage welder.
This makes flux-core wire a practical choice for maximizing 1/4-inch MIG welding performance on 110V equipment. The wire feeder ensures a steady supply of filler metal, maintaining consistent weld quality during operation.
Along with enhancing penetration, flux-core wire markedly reduces weld defects on 1/4-inch steel when using a 110V MIG welder.
You’ll see fewer porosity issues and improved slag coverage, which stabilizes the weld pool. This minimizes the risk of incomplete fusion and undercut, common problems on thicker material at lower amperage.
Specifically, flux-core wire:
Using flux-core wire helps you achieve cleaner, stronger welds on 1/4-inch steel with a 110V MIG setup. Additionally, flux-cored wire offers higher deposition rates compared to solid wire, which can speed up welding on thicker materials.
Choosing flux-core wire markedly eases the challenges of welding 1/4-inch steel with a 110V MIG machine by enhancing arc stability and heat transfer.
You’ll find that flux-core wire generates a hotter, more concentrated arc, which improves penetration on thicker material within the limited amperage range of 110V welders.
This results in better fusion and fewer cold lap defects compared to solid wire. Additionally, the flux provides shielding gas internally, eliminating the need for external gas and reducing porosity risks in less controlled environments.
While flux-core doesn’t replace the power advantages of a 220V machine, it optimizes your 110V setup by allowing more consistent multi-pass welds on 1/4-inch steel.
Employing flux-core wire is a practical approach to overcoming typical 110V limitations without upgrading voltage. Using self-shielded flux-cored wire also means you can weld effectively outdoors or in windy conditions due to the internal gas generation.
Because 110V MIG welders often have a low duty cycle at maximum output, managing heat effectively becomes critical when welding 1/4-inch steel.
Effective heat management is essential when welding 1/4-inch steel with 110V MIG welders.
You need to avoid overheating the machine and the workpiece, which can cause warping or equipment shutdown.
To optimize heat management and duty cycle, follow these key steps:
Also, adjusting your wire feed speed and voltage carefully can help maintain a stable arc and reduce unnecessary heat buildup during welding.
Frequently, you’ll find that welding 1/4-inch steel demands more power and consistency than a 110V MIG welder can reliably provide.
When you need deeper penetration, longer continuous welds, or frequent work on thicker material, 220V offers a clear advantage.
It supports higher amperage, improves duty cycle, and delivers steady heat input. This reduces the risk of weak welds or overheating.
| Factor | 110V MIG |
|---|---|
| Max Amperage | Up to ~140 amps |
| Duty Cycle | Limited at high output |
| Penetration | Marginal on 1/4-inch |
| Continuous Welding | Restricted by heat build-up |
| Setup Complexity | Requires beveling, multi-pass |
Choose 220V when you prioritize weld quality, efficiency, and durability on 1/4-inch steel. Typical amperage for 1/4-inch steel MIG welding with 0.035 wire is around 180–220 amps, which 110V machines generally cannot sustain.
Welding 1/4-inch steel with a 110V MIG welder can be a bit tricky, but with the right techniques, you can get great results.
First off, let’s talk about joint preparation. It’s super important to bevel the edges and clean the surfaces thoroughly. This step is crucial because it helps ensure a solid fusion when you start welding.
Now, once you’re set up, you’ll want to adjust your machine carefully. Getting the wire speed and voltage just right within your welder’s limits is key. This will really help with penetration and the overall quality of your bead.
And don’t forget about the multi-pass strategy. It’s a great way to manage heat input, which is especially important for thicker materials like 1/4-inch steel. By layering your welds, you can achieve stronger and more reliable results.
Keep in mind that 110V machines typically handle mild steel up to about 1/4 inch thickness, making them suitable for these projects.
Happy welding!
When preparing joints for welding 1/4-inch steel with a 110V MIG welder, prioritize beveling the edges to guarantee adequate penetration and fusion. Without proper beveling, your welds risk being weak or incomplete due to the limited heat input of a 110V machine.
Beyond beveling, meticulous joint preparation is essential for success.
Consider these key steps:
Following these techniques helps overcome 110V limitations and achieves reliable welds on 1/4-inch steel.
After properly preparing and beveling your joint for 1/4-inch steel, fine-tuning your 110V MIG welder’s settings becomes the next step to maximize penetration and weld quality.
Start by setting your voltage near the upper limit the machine allows, typically around 18–20 volts for 1/4-inch steel. Adjust wire feed speed to match voltage, aiming for a stable, consistent arc without spatter.
Use a 0.030-inch wire diameter to balance penetration and control. Set your travel speed slow enough to allow proper fusion but avoid excessive heat buildup that can cause warping.
Opt for a shielding gas mix with at least 75% argon to stabilize the arc and reduce oxidation. Finally, maintain a short arc length of about 1/8 inch to optimize heat transfer, critical given the 110V machine’s limited amperage and duty cycle.
Mastering a multi-pass welding strategy is essential for achieving sound, deep penetration welds on 1/4-inch steel with a 110V MIG welder.
Since these machines often provide marginal heat output, layering weld passes guarantees sufficient fusion and strength.
You should prepare the joint with a bevel to facilitate access to the root.
To execute a precise multi-pass weld, focus on:
This technique compensates for limitations in amperage and duty cycle inherent in 110V machines.
You need a welding helmet with a proper shade to protect your eyes from intense UV and infrared light.
Wear flame-resistant gloves and a long-sleeve jacket to shield your skin from sparks and heat.
Use safety boots and pants made of non-flammable material to prevent burns.
Respiratory protection is essential if ventilation is poor since fumes increase with thicker steel and multiple passes.
Always make sure your workspace is clear and well-ventilated.
Think of your 110V MIG welder as a versatile brush, capable but limited by canvas size.
You can weld metals like mild steel, light gauge stainless steel, and some thin aluminum with the right wire and shielding gas.
However, its power and duty cycle constrain you mainly to thinner materials.
For thicker or exotic metals, you’ll need higher amperage or specialized machines.
Always match your setup to the metal’s thermal properties for clean, strong welds.
Wire diameter directly impacts your ability to weld 1/4-inch steel with a 110V MIG.
Thicker wire, like .035-inch, provides better heat input and penetration compared to thinner .023-inch wire. This helps you achieve stronger welds on thicker material.
However, larger wire demands more amperage, which strains lower-powered 110V machines.
You’ll need to balance wire size with machine capacity and adjust voltage and wire feed speed carefully for the best multi-pass welding results.
If you get poor welds on 1/4-inch steel, start by checking your joint prep. Make sure bevels are clean and fit-up is tight.
Adjust wire speed and voltage to avoid burn-through or insufficient fusion. Use multiple passes with adequate cooling to prevent warping and overheating.
Inspect your ground connection for stability and guarantee proper wire diameter and feed rate. Clean the metal thoroughly to remove rust or contaminants that weaken the weld.
Think of ambient temperature and humidity as the weather steering your welding ship.
Cold temps make your 110V MIG’s arc unstable, causing poor fusion and spatter. High humidity invites moisture that leads to weld porosity and weak joints.
You need consistent, dry conditions to keep your arc steady and penetration reliable.
Managing these factors means better weld quality, especially since 110V MIGs already operate near their performance limits on thicker steel.
Welding 1/4-inch steel with a 110V MIG welder is like steering a compact boat through deep waters. You can navigate, but the currents demand respect.
You’ll need precise joint prep, controlled heat, and patience with multi-pass techniques to keep your welds strong and consistent.
While 110V can handle the task, sometimes upgrading to 220V is the lighthouse guiding you through tougher jobs. It ensures power and stability when your project’s depth truly calls for it.