Phone:
(701)814-6992
Physical address:
6296 Donnelly Plaza
Ratkeville, Bahamas.

Phone:
(701)814-6992
Physical address:
6296 Donnelly Plaza
Ratkeville, Bahamas.
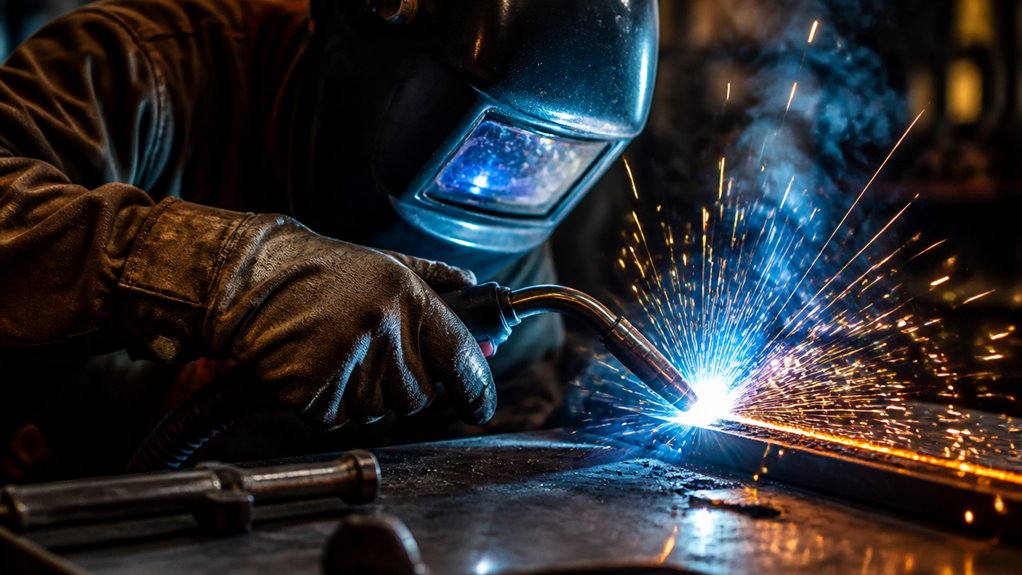
MIG welding isn’t hard if you focus on mastering gun angle, travel speed, and proper machine settings early on.
The automatic wire feed helps you concentrate on technique rather than manually feeding filler material.
Beginners can achieve acceptable flat-position beads within hours, though overhead and vertical positions require more skill.
Clean base metal and correct shielding gas are essential for strong welds.
Understanding your machine’s settings and setup will markedly reduce spatter and weak welds.
Discover how these factors influence your welding quality next.
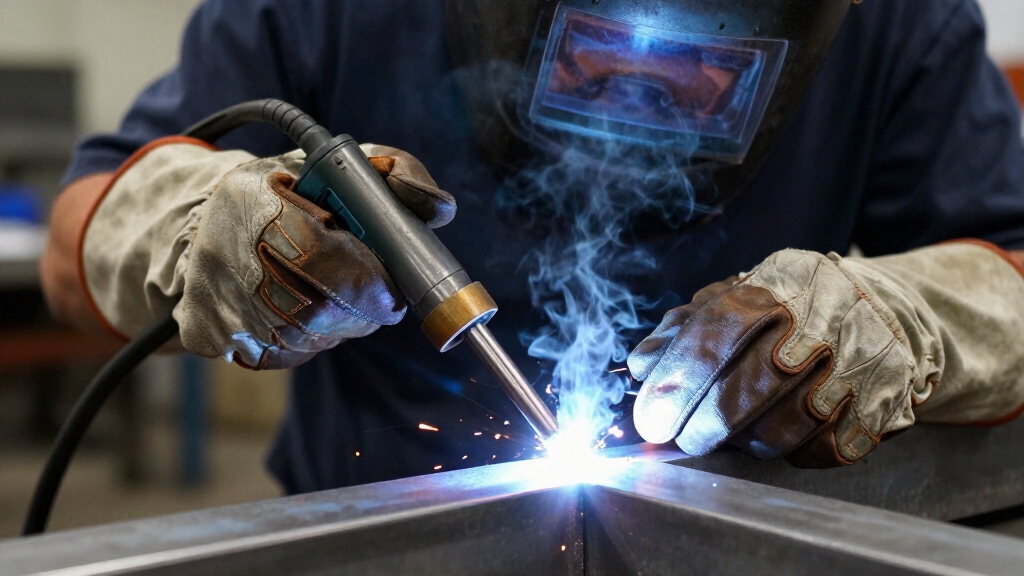
MIG welding stands out as an accessible entry point because it takes much of the manual complexity out of the equation by automatically feeding the wire.
MIG welding simplifies the process by automating wire feeding, making it an ideal starting point for beginners.
This automation removes the need to manually feed filler material, letting you focus on maintaining proper gun angle and travel speed.
Within your initial practice hours, you can produce acceptable flat-position beads, unlike more intricate processes like TIG welding, which demand higher dexterity and control.
Although the machine simplifies wire delivery, you still have to verify correct voltage and wire-feed settings to stabilize the arc.
Clean base metal and consistent gas flow are also critical for quality welds.
Proper wire feed speed adjustment is essential to avoid common issues like spatter and poor penetration.
You know, one of the biggest issues with MIG welding is getting the voltage and wire-feed settings just right. If they’re off, you might end up with weak welds and a lot of spatter, which really messes with the overall quality.
Now, let’s talk about the metal surface. If there are contaminants like rust or oil, they can really throw a wrench in the works. These impurities interfere with arc stability, making it tough to achieve good fusion and leading to defects.
And don’t forget about the gun angle! Maintaining the right angle is super important. If you’re not controlling it well, you could end up with porosity and inconsistent bead formation, which are definitely not what you want.
Fine-tuning parameters like voltage and wire feed based on arc sound cues can help you achieve a more stable and clean weld.
Although the welding machine automates wire feeding, incorrect voltage and wire-feed settings remain a primary cause of weak welds and excessive spatter.
You need to balance these parameters carefully: too high wire-feed speed overwhelms the arc, causing excessive spatter and poor bead shape. Too low speed leads to insufficient penetration and cold welds.
Voltage directly affects arc length and heat input. Setting it too high causes burn-through and undercut, while too low voltage produces unstable arcs and lack of fusion.
Adjusting voltage and wire feed together is critical because they interact. Raising voltage often requires increasing wire feed to maintain a stable arc.
Proper calibration demands iterative testing, paying close attention to bead appearance and penetration to optimize weld quality and arc stability.
Matching the wire diameter with amperage is essential to ensure arc stability and reduce welding defects.
Setting the correct voltage and wire-feed speeds guarantees the arc behaves properly. However, even a perfectly tuned machine can’t compensate for metal surface contaminants.
When welding over rust, oil, paint, or dirt, you risk introducing porosity and weak fusion into the weld. Contaminants disrupt the molten pool’s stability and cause inconsistent arc behavior, leading to spatter and poor bead formation.
Before you start, thoroughly clean the base metal using mechanical methods like wire brushing or grinding. Ensure a bright, contaminant-free surface. Residual oils or mill scale require degreasing or chemical cleaning.
Neglecting this step often results in weld defects that weaken the joint and compromise structural integrity. Maintaining strict metal cleanliness is a non-negotiable prerequisite for producing sound, high-quality MIG welds consistently.
For rusted metal, it is critical to grind off heavy rust and clean thoroughly to avoid porosity and weak fusion in the weld.
Mastering gun angle control plays a critical role in producing strong, defect-free MIG welds. You need to keep the gun angle within a narrow range, typically 0 to 15 degrees from vertical, to guarantee proper penetration and bead shape.
Deviating too much causes uneven heat distribution, leading to defects such as porosity, lack of fusion, or burn-through. Consistency in maintaining this angle while moving the gun steadily is key to avoiding weak spots.
Additionally, controlling the wire stickout, usually no more than ½ inch past the nozzle, stabilizes the arc and improves weld quality. Poor gun angle control disrupts gas shielding coverage, increasing the risk of contamination and spatter.
Using the correct shielding gas mixtures is essential to maintain gas coverage and prevent weld defects during MIG welding.
To set up your MIG welder for success, the first thing you want to do is make sure the base metal is squeaky clean. That means getting rid of any rust, paint, or oils. If you skip this step, you could end up with contamination, which is definitely not what you want.
Next up, let’s talk about the shielding gas flow. You’ll need to adjust it to the right rate. If the coverage isn’t spot on, you might run into issues like porosity and weak welds. And nobody wants that, right?
Finally, you’ve got to calibrate the voltage and wire feed speed. This part is crucial! Make sure they match the material thickness and wire diameter perfectly. When everything is dialed in just right, you’ll achieve stable arc performance and optimal penetration. Happy welding!
Remember to attach the ground clamp to clean, bare metal close to the weld area to minimize resistance and voltage drop for a smooth welding process.
Making sure your base metal is thoroughly clean is critical for achieving strong, defect-free MIG welds. Contaminants like rust, paint, oil, and dirt interfere with arc stability and penetration, causing porosity, weak fusion, and spatter.
Before welding, remove all surface impurities using mechanical methods such as wire brushing, grinding, or sanding. For oily residues, use a suitable solvent or degreaser.
Inspect the metal closely to confirm complete cleanliness, especially at joint edges where contaminants concentrate. Neglecting this step results in weld defects that compromise joint strength and aesthetics.
Consistently clean base metal ensures the shielding gas fully protects the molten pool from atmospheric contamination. This foundational preparation reduces troubleshooting and rework, making your MIG welding process more efficient and reliable.
Cleanliness directly correlates with weld quality and consistency. Proper gas flow rates prevent contamination while avoiding turbulence to maintain weld integrity and appearance during the welding process, which is essential for high-quality shielding gas protection.
Correct gas flow consistently plays a critical role in stabilizing the welding arc and protecting the molten weld pool from contamination.
If your shielding gas flow is incorrect, you risk porosity, oxidation, and weak welds.
To set up your MIG welder properly, focus on these key points:
Adjust flow rate typically between 15-25 cubic feet per hour (CFH), depending on your environment and material thickness.
Make certain your gas regulator and flowmeter are calibrated and leak-free.
Use the right gas mixture, commonly 75% argon and 25% CO2 for mild steel, to balance arc stability and penetration.
Check for proper gas nozzle condition and positioning to maintain consistent shielding coverage.
Balancing blends and adjusting flow rates achieves consistent, clean, controlled cuts with improved arc stability.
A stable arc and strong welds depend heavily on setting the proper voltage on your MIG welder.
Voltage controls the arc length and heat input. Too low, and you get a cold weld with poor penetration. Too high, and you risk burn-through and excessive spatter.
To set voltage correctly, refer to the welder’s chart for your wire diameter and material thickness.
Adjust incrementally while observing the arc’s behavior, aiming for a smooth, consistent bead with minimal spatter.
Remember, voltage interacts with wire feed speed, so calibrate both together for peak results.
Maintaining proper voltage guarantees arc stability, proper fusion, and bead appearance.
Consistently monitor and fine-tune voltage as conditions change, such as material type or weld position, to achieve repeatable, high-quality welds.
Using the Auto-Set feature can simplify the process by automatically adjusting voltage and wire feed speed based on material thickness and wire diameter.
When you weld with contaminated metal, the resulting bond weakens and often becomes porous, compromising structural integrity.
Welding contaminated metal weakens bonds and creates porosity, undermining structural strength.
Dirt, rust, oil, and paint create barriers that prevent proper fusion, leading to defects.
Similarly, using incorrect shielding gas or insufficient flow allows atmospheric gases like oxygen and nitrogen to contaminate the weld pool, causing porosity and brittleness.
To guarantee consistent, strong welds, focus on:
Using the right shielding gases also strongly influences arc stability, heat input, and weld quality.
Mastering clean metal and proper shielding gas sets the foundation, but many beginners still run into avoidable errors that undermine weld quality. You might forget to open the shielding gas valve or select the wrong gas mixture, causing porosity and weak welds.
Incorrect wire feed speed disrupts bead shape. Too high results in excessive spatter, while too low leads to poor penetration. Voltage settings also demand precision. Excessive voltage causes burn-through, while insufficient voltage produces cold, underfused welds.
Welding over dirty or contaminated surfaces frequently leads to weak joints riddled with inclusions. Consistency is key; irregular travel speed or stopping can create uneven beads and internal defects.
Since gun angle and travel speed directly influence weld bead formation and penetration, controlling them precisely is essential for quality MIG welds.
Holding the gun at a consistent angle, typically 0 to 15 degrees from vertical, ensures stable arc length and uniform bead shape.
Travel speed controls heat input. Moving too fast reduces penetration and causes a narrow bead, while moving too slow leads to excessive buildup and burn-through.
Inconsistent gun angle or speed often results in porosity, undercut, or lack of fusion.
Key effects to monitor include:
Controlling gun angle and travel speed lays the foundation for producing consistent welds. Choosing the right welding position can make your initial practice more manageable.
The flat position is the easiest for beginners because gravity assists in puddle control and visibility is optimal. You’ll find lap joints, butt joints, and horizontal tee joints ideal as they allow steady movement without complex manipulation.
Avoid overhead and vertical positions initially; they demand superior puddle control and consistent travel speed, increasing difficulty. Flat welding lets you focus on mastering machine settings and hand coordination before tackling positional challenges.
Starting in flat position helps you build confidence and repeatability. This reduces early errors linked to poor control or unstable arcs. Progressing methodically guarantees your foundational skills solidify efficiently.
Although MIG welding is accessible for beginners, avoiding weak welds and excessive spatter requires careful attention to machine settings and material preparation.
You need to make certain your base metal is clean and free from rust, oil, or paint, as contaminants cause porosity and poor fusion.
Adjust your voltage and wire feed speed precisely to maintain arc stability and proper penetration.
Keep the gun angle between 0 to 15 degrees and limit wire stickout to around ½ inch to prevent erratic arcs and spatter.
Thoroughly clean the welding surface before starting.
Set shielding gas flow correctly and verify gas type.
Calibrate voltage and wire feed speed to match material thickness.
Maintain consistent gun angle and travel speed.
These steps directly reduce weak welds and spatter formation.
Maintaining clean metal, proper gas flow, and correct machine settings lays the foundation. Achieving consistent, reliable MIG welds also depends on disciplined technique. You must control travel speed, gun angle, and wire stickout precisely to avoid defects like porosity and weak penetration.
Repeatable setup and steady hand movement guarantee uniform bead appearance and strength.
| Parameter | Ideal Range | Effect of Deviation |
|---|---|---|
| Gun Angle | 0° to 15° | Increased spatter, poor fusion |
| Wire Stickout | ≤ 1/2 inch | Arc instability, weak weld |
| Travel Speed | Consistent, moderate | Burn-through or cold welds |
| Voltage & Feed | Per material spec | Porosity, excessive spatter |
Master these factors for dependable MIG welding results every time.
You can use MIG welding on a variety of metals, including mild steel, stainless steel, and aluminum.
It works best on clean, flat surfaces with proper shielding gas tailored to each metal type: argon or argon mixes for aluminum and stainless, and CO2 or argon-CO2 blends for mild steel.
While MIG handles thin to moderately thick materials well, you’ll need to adjust settings carefully depending on the metal’s thickness and alloy composition.
A typical MIG welding wire spool lasts about 15 to 25 pounds of wire, translating roughly to 200 to 300 feet, depending on wire diameter and type.
If you weld continuously at a moderate speed, expect a spool to last several hours of work.
Your actual usage varies with welding current, joint type, and technique.
Keep track of wire feed speed and amperage to optimize spool life and maintain consistent weld quality.
Yes, you can do MIG welding outdoors, but windy conditions pose challenges.
Wind disrupts shielding gas coverage, causing porosity and weak welds. To mitigate this, you should use windshields, increase gas flow slightly, or switch to flux-cored wire, which doesn’t need shielding gas.
Always prioritize clean metal and stable settings to maintain arc quality. Without these precautions, wind will degrade weld strength and appearance markedly.
You need a welding helmet with a proper shade to protect your eyes from intense UV radiation. Over 90% of eye injuries in welding come from inadequate protection.
Wear flame-resistant gloves and a long-sleeve jacket to shield your skin from sparks and heat. Respiratory protection is essential if ventilation is poor, preventing inhalation of toxic fumes.
Don’t forget ear protection for noise and safety boots to guard against heavy objects or molten metal.
If your MIG welder won’t start, first check the power supply and make certain it’s plugged in and switched on.
Inspect the circuit breaker and fuses for faults.
Verify that the gas cylinder valve is open and the regulator is set correctly.
Examine the trigger switch and wiring for damage or loose connections.
Also, confirm the ground clamp is securely attached to clean metal.
Addressing these points usually resolves startup issues effectively.
As you grasp the torch, envision each weld bead as a precise stitch weaving metal securely.
While MIG welding poses challenges like maintaining the right gun angle and clean surfaces, mastering these technical details transforms complexity into control.
By fine-tuning your setup and technique, you’ll consistently produce strong, spatter-free welds.
With practice, what once seemed intimidating becomes a reliable process, turning raw materials into seamless, durable structures with analytical precision.