Phone:
(701)814-6992
Physical address:
6296 Donnelly Plaza
Ratkeville, Bahamas.

Phone:
(701)814-6992
Physical address:
6296 Donnelly Plaza
Ratkeville, Bahamas.
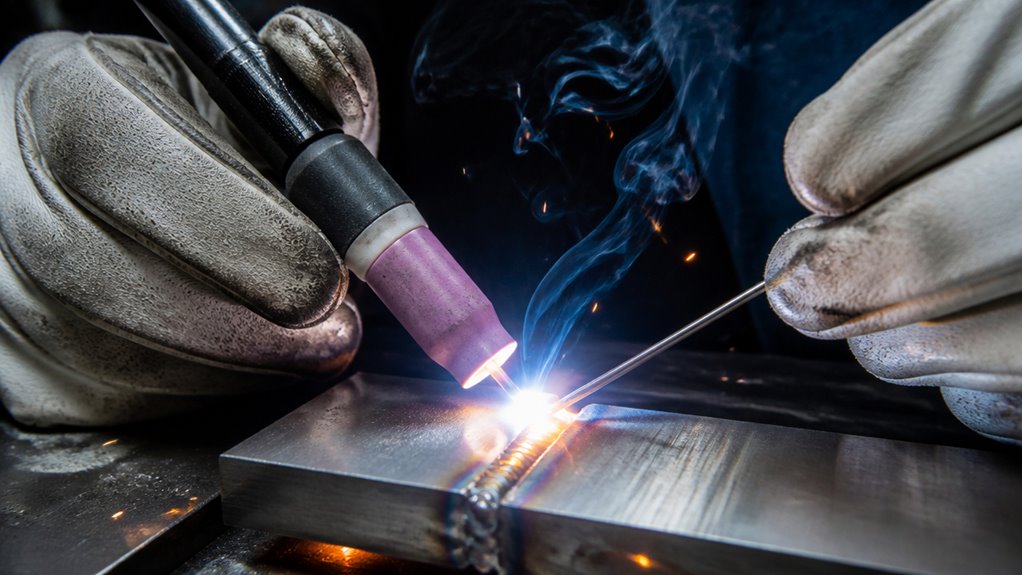
Gas tungsten arc welding (GTAW), also called TIG welding, lets you create precise, high-quality welds using a non-consumable tungsten electrode to generate a stable arc.
You’ll use inert gases like argon or helium to shield the weld pool from contamination, ensuring clean fusion and minimal distortion.
This process suits thin, reactive, and corrosion-resistant metals, giving you excellent heat control and weld integrity.
Understanding GTAW’s equipment, gas roles, and material compatibility further enhances your results.
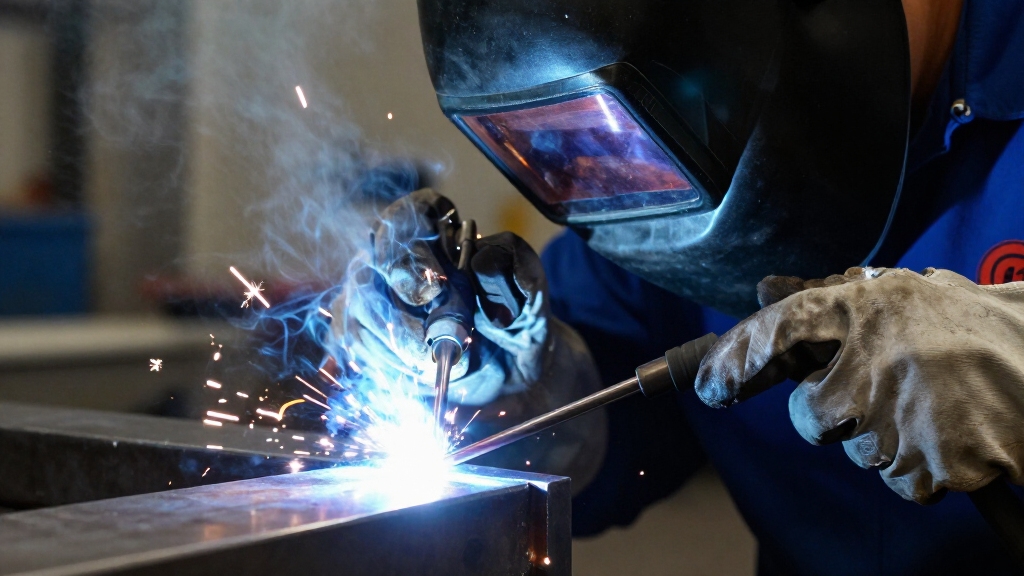
Gas tungsten arc welding (GTAW), also known as tungsten inert gas (TIG) welding, uses a non-consumable tungsten electrode to generate an arc that melts the base metal and forms a high-quality weld joint.
Gas tungsten arc welding (GTAW) employs a tungsten electrode to create precise, high-quality welds by melting base metal.
You rely on an inert shielding gas, typically argon or helium, to protect this weld zone from atmospheric contamination, ensuring weld integrity.
GTAW classifies as a fusion welding process because it melts the base metal without consuming the electrode.
It excels in applications demanding clean, precise welds, such as stainless steel or aluminum fabrication.
You may add filler metal separately, but it’s not always necessary.
The process’s precision and cleanliness make it indispensable where joint quality directly impacts performance, including aerospace and nuclear industries.
Your control of heat input and shielding gas flow directly influences weld consistency and strength.
The arc is initiated via a high-frequency generator without electrode contact, allowing for controlled heat input and precise bead formation.
Understanding the mechanics behind GTAW helps clarify why it achieves such clean, high-quality welds.
You initiate the process by establishing an arc between a non-consumable tungsten electrode and the workpiece.
The intense arc heat precisely melts the base metal, creating a controlled weld pool.
You may add filler metal separately if the joint requires additional material, but the tungsten electrode itself remains intact, preventing contamination.
A constant flow of inert shielding gas envelops the weld zone, protecting it from atmospheric gases like oxygen and nitrogen that cause oxidation and defects.
Your control over arc stability, heat input, and shielding guarantees a clean fusion weld with minimal spatter.
This precision welding method suits applications demanding impeccable joint integrity and metallurgical soundness.
Precise arc intensity control, often via a foot pedal, allows dynamic adjustment during welding to produce consistent, professional results.
A well-configured welding setup relies on several key components to guarantee precise control and consistent results in GTAW. You need a welding power source to supply a stable current, a torch to hold the tungsten electrode and direct shielding gas, and a flowmeter regulator to control gas flow precisely.
Tungsten electrodes themselves are critical; their shape influences arc stability and weld quality. Additionally, filler rods come into play when extra material is required.
| Equipment | Function | Importance |
|---|---|---|
| Power Source | Supplies current for arc | Secures stable and consistent arc |
| Torch | Holds electrode, directs gas | Controls heat and shielding |
| Flowmeter Regulator | Regulates shielding gas flow | Maintains protective atmosphere |
| Tungsten Electrodes | Non-consumable arc conductor | Provides arc stability |
Proper selection and control of the shielding gas is essential to prevent oxidation and contamination during welding.
This equipment forms the foundation for efficient GTAW operation.
You know, when you’re using GTAW, shielding gas plays a crucial role. It creates this inert atmosphere that really helps prevent oxidation and contamination. Without it, your welds could end up looking pretty rough!
Now, common gases like argon and helium—or even mixtures of them—can have a big impact on how stable your arc is and how deep your weld penetration goes. It’s pretty fascinating, right?
Selecting the right shielding gas mixture is essential to optimize arc stability, heat input, and weld quality for different materials and joint designs.
Shielding gas plays a critical role in maintaining the integrity of a GTAW weld by protecting the molten weld pool and tungsten electrode from atmospheric contamination. Without this protection, oxygen, nitrogen, and hydrogen from the air would react with the hot metal, causing defects like porosity, oxidation, and embrittlement.
When you use shielding gas, it creates an inert or semi-inert environment that stabilizes the arc and preserves weld quality. Key functions include:
Argon is the most commonly used shielding gas in GTAW because it provides excellent arc stability and a protective cloak for the welds.
Selecting the appropriate gas type directly influences the stability and quality of GTAW welds. You typically use argon, helium, or their mixtures as shielding gases. Argon offers excellent arc stability and is ideal for most metals. Helium increases heat input and penetration but can cause a less stable arc. Mixing gases balances these effects for specific applications.
| Gas Type | Characteristics | Typical Use |
|---|---|---|
| Argon | Stable arc, good shielding | Stainless steel, aluminum |
| Helium | Higher heat, deeper weld | Thick materials, aluminum |
| Argon-Helium Mix | Balanced heat and stability | Versatile, specialty alloys |
Choosing the right gas guarantees effective protection from atmospheric contamination. This helps maintain weld integrity. Argon’s ability to provide an inert atmosphere ensures the molten metal is shielded from oxygen and nitrogen, preventing contamination and defects.
Although the tungsten electrode generates the arc heat, the shielding gas plays a crucial role in preserving weld quality. It prevents atmospheric gases like oxygen and nitrogen from contaminating the molten weld pool. Without proper shielding, these gases can induce porosity, oxidation, and embrittlement, compromising weld integrity.
You rely on the shielding gas to maintain a stable arc and clean weld surface. This directly impacts mechanical properties and corrosion resistance. Key effects of shielding gas on GTAW weld quality include:
Controlling shielding gas flow and composition is essential to achieving peak weld performance in GTAW. Oxygen is highly reactive and cannot serve as a shielding gas as it promotes oxidation and weld contamination, weakening weld integrity.
Deciding when to use filler metal in GTAW depends on the joint design, material thickness, and desired weld properties.
You’ll add filler metal primarily to guarantee adequate joint strength, fill gaps, or control weld bead shape.
Thin materials or butt joints often require no filler, while thicker or complex joints benefit from added metal to prevent defects and improve mechanical properties.
| Joint Type | Material Thickness | Filler Metal Use | Reason |
|---|---|---|---|
| Butt Joint | Thin (<3 mm) | No | Fusion only sufficient |
| Butt Joint | Thick (>3 mm) | Yes | Fill large gaps |
| Lap Joint | Any | Yes | Ensure full penetration |
| Corner Joint | Medium to Thick | Yes | Strengthen weld area |
| Edge Joint | Thin | No | Minimal reinforcement needed |
Use filler metal strategically to optimize weld integrity and performance. Proper torch angle and consistent feeding technique are essential to achieve clean and strong welds when using filler metal.
When determining the most suitable materials for GTAW welding, consider the process’s strengths in producing clean, high-quality joints with precise heat control.
GTAW excels on metals that require minimal contamination and fine thermal management. You’ll find it especially effective on reactive and corrosion-resistant alloys.
Materials best suited for GTAW include:
Choosing these materials leverages GTAW’s ability to maintain weld integrity and metallurgical properties without compromising quality. For aluminum welding, an AC-capable TIG welder is essential to effectively remove oxide layers and achieve proper fusion.
When you’re using GTAW, one of the key things you rely on is that shielding gas. It plays a crucial role in protecting the weld pool from any atmospheric contamination.
This way, you create a clean environment for fusion, which is essential for a strong weld.
Now, let’s talk about the tungsten electrode. It’s non-consumable, which means it doesn’t melt away during the process.
This helps maintain a stable arc without introducing any impurities. Pretty neat, right?
And then there’s the control over heat input. By managing that carefully, you can prevent distortion and really nail down those consistent, high-quality welds.
It’s all about precision!
Using 2% ceriated tungsten (WC20) can provide peak arc stability when welding aluminum alloys, enhancing the overall weld quality.
Consistently maintaining an effective shielding gas environment is essential to ensuring the cleanliness and integrity of GTAW welds. This inert gas envelops the weld pool, preventing atmospheric gases like oxygen, nitrogen, and hydrogen from contaminating the molten metal.
If contamination occurs, oxidation and porosity can weaken the weld. You control shielding gas flow rate and composition precisely to achieve peak protection.
Key factors to manage include:
Maintaining an uncontaminated weld environment depends not only on shielding gas but also on the non-consumable tungsten electrode. This electrode plays a fundamental role in GTAW’s ability to produce clean, high-quality welds.
It remains solid during welding, preventing contamination from electrode melting and ensuring a stable, focused arc. Its high melting point and excellent electrical conductivity enable consistent arc initiation and maintenance, vital for precise heat control.
You must select the appropriate tungsten type and grind it to a specific shape to optimize arc stability and penetration. By avoiding electrode consumption, GTAW minimizes spatter and impurities in the weld pool, reducing defects.
Ultimately, the tungsten electrode’s durability and performance are key to achieving the process’s hallmark of clean, precise, and defect-free welds.
Controlling heat input precisely during GTAW is crucial for producing clean, high-quality welds. You regulate the arc’s intensity carefully, preventing excessive melting or distortion of the base metal. This precision minimizes thermal stress and guarantees a sound fusion without compromising the material’s integrity.
To maintain peak heat input, you must:
This meticulous control reduces oxidation and spatter, resulting in welds that meet stringent quality standards, especially for critical applications requiring flawless joints.
Although GTAW operates at a slower pace than some other welding methods, it gives you unmatched control over heat input and weld quality. This enables the production of exceptionally clean joints with minimal spatter.
This precision makes GTAW ideal for welding thin sections and reactive metals like aluminum and stainless steel, where contamination and distortion must be minimized. Unlike consumable electrode processes, GTAW uses a non-consumable tungsten electrode, which helps maintain consistent arc stability and reduces welding defects.
Additionally, the inert shielding gases prevent oxidation effectively, ensuring superior metallurgical properties. You’ll also appreciate GTAW’s versatility; it works well in all welding positions and supports both autogenous and filler metal welding.
This makes it suitable for critical applications demanding high integrity and aesthetic finish.
When you weld using GTAW, you face challenges that demand meticulous attention to detail and strict safety protocols. The process requires you to maintain clean surfaces and precise gas coverage to avoid oxidation and weld defects.
You must coordinate torch manipulation, filler addition, and heat input with skill to guarantee strong, high-quality joints. Additionally, you need to protect yourself rigorously against hazards like UV radiation and hot metal.
Keep these safety tips in mind:
Always wear proper PPE, including welding helmets with UV protection and flame-resistant clothing. Guarantee adequate ventilation to prevent inhalation of harmful fumes.
Regularly check shielding gas flow and connections for leaks or blockages. Handle tungsten electrodes carefully to avoid contamination that impairs arc stability.
Following these guidelines helps you mitigate risks and maintain weld integrity.
To improve GTAW weld quality, it’s really important to optimize the shielding gas flow. This ensures that the weld pool is completely protected from atmospheric contamination. Nobody wants that, right?
Now, let’s talk about electrode preparation. Proper shaping and cleaning of the electrode are crucial for maintaining stable arc control and achieving consistent welds. Trust me, focusing on these aspects can significantly reduce defects.
In the end, paying attention to these factors not only enhances joint integrity but is especially vital for critical applications. So, let’s make sure we get it right!
Effective shielding gas optimization plays a crucial role in improving GTAW weld quality by ensuring consistent protection of the weld pool from atmospheric contamination.
To optimize shielding gas, you must control flow rate, gas composition, and delivery to maintain a stable arc and prevent oxidation.
You’ll want to contemplate adjusting flow rates to avoid turbulence and gas wastage.
Selecting appropriate gas mixtures like pure argon or argon-helium blends is essential for material compatibility.
Ensuring proper nozzle design and size is vital for effective gas coverage.
Additionally, minimizing environmental factors such as wind or drafts can help maintain a stable gas shield.
Optimizing shielding gas sets the stage for stable arc conditions. However, maintaining weld quality also hinges on proper electrode preparation techniques.
You must shape the tungsten electrode tip to ensure a focused, stable arc. Use a dedicated grinder with a fine-grit wheel, grinding longitudinally along the electrode’s axis to avoid contamination and irregular arc behavior.
Avoid touching the electrode with bare hands, as oils and dirt can degrade performance. For DC welding, a pointed tip improves arc precision.
AC welding on aluminum often requires a balled tip to enhance arc stability. Consistently inspect the electrode for oxidation or damage and replace it when necessary.
To choose the right tungsten electrode type and size, consider the welding current, material, and polarity.
For AC welding on aluminum, use pure tungsten or zirconiated electrodes. For DC welding on steel or stainless, use thoriated or ceriated tungsten.
Match electrode diameter to current. Smaller diameters suit lower amps for precision, while larger diameters handle higher amps.
Always select tungsten graded for your welding conditions to ensure arc stability and longevity.
To keep your GTAW torch in prime shape, routinely inspect and gently refresh its components.
Clean the nozzle and gas lens to guarantee consistent shielding gas flow.
Check the tungsten electrode for proper sharpness and positioning.
Replace worn or damaged parts promptly to maintain arc stability and weld quality.
Regularly examine cables and connections for wear to avoid electrical issues.
This ensures your torch performs with precision and reliability every time.
Yes, you can automate GTAW for large-scale production, but it demands precise control systems due to its intricate parameters.
Automation improves consistency and speed, especially in industries like aerospace and automotive.
You’ll need robotic arms equipped with accurate torch positioning, advanced sensors for arc stability, and integrated filler wire feeding mechanisms.
However, the process’s slower welding speed compared to other methods means you must balance throughput with weld quality carefully.
Oh, you just love spending extra on welding, don’t you?
GTAW’s cost is higher upfront. Equipment, shielding gas, and skilled labor add up.
Compared to MIG or stick welding, it’s pricier due to slower speed and precision demands.
But if you want spotless, high-quality welds on tricky metals, it’s worth every penny.
You pay more for excellence, control, and minimal cleanup.
Common GTAW defects include tungsten inclusion, porosity, and lack of fusion.
You can fix tungsten inclusion by maintaining proper electrode extension and angle.
Porosity often results from poor shielding gas coverage, so make certain gas flow is adequate and uncontaminated.
Lack of fusion occurs if heat input is too low or torch manipulation is poor; adjust amperage and technique to improve penetration.
Cleanliness and precise control are key to preventing these defects.
Mastering Gas Tungsten Arc Welding lets you achieve welds as precise and clean as a surgeon’s incision. By understanding its equipment, shielding gases, and filler metal use, you control every variable for superior quality.
While challenges exist, following safety protocols and refining your technique will enhance your results. Embracing GTAW’s advantages empowers you to produce durable, high-integrity welds critical in demanding applications where precision is non-negotiable.