Phone:
(701)814-6992
Physical address:
6296 Donnelly Plaza
Ratkeville, Bahamas.

Phone:
(701)814-6992
Physical address:
6296 Donnelly Plaza
Ratkeville, Bahamas.
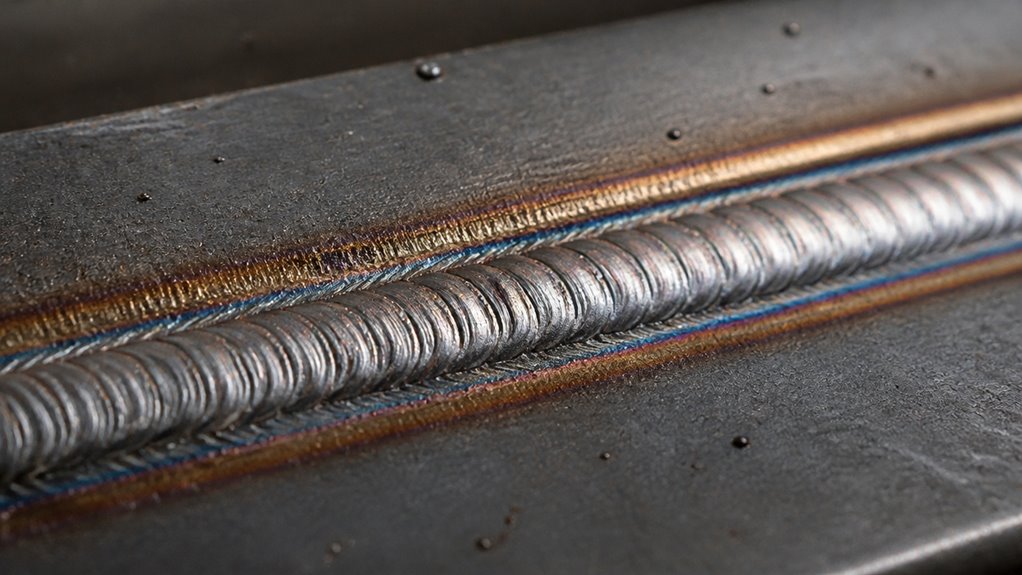
You can spot a good stick weld by its smooth, uniform bead that precisely follows the joint line without wandering or abrupt edges.
It has balanced height and width with regular ripples, indicating stable travel speed and heat control.
You won’t see surface defects like porosity, undercut, or overlap.
The weld’s toe blends gradually with the base metal, ensuring solid fusion and strength.
While visual signs matter, understanding deeper aspects can help you recognize full weld quality.
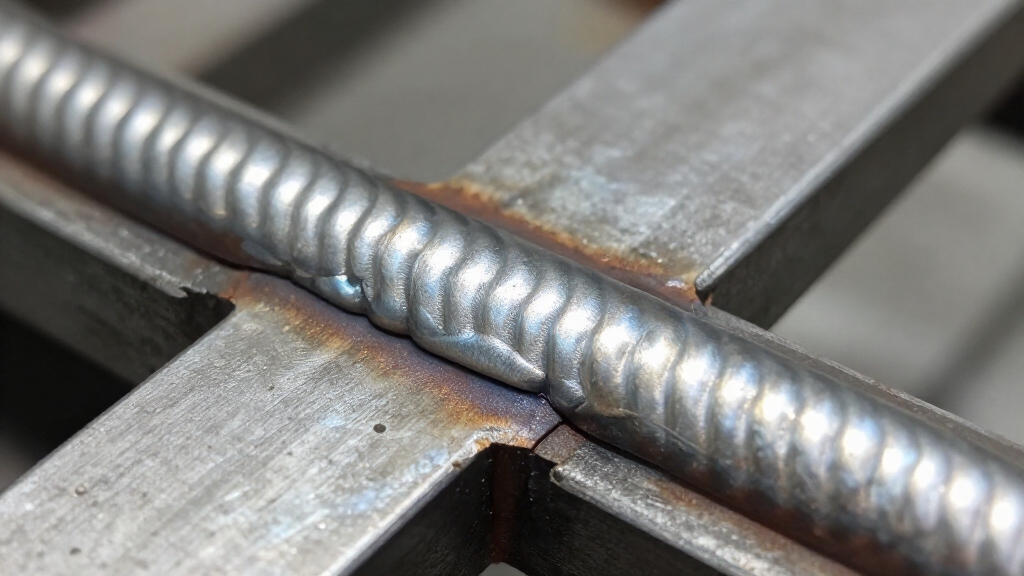
Spotting a good stick weld starts with examining its consistency and control along the joint.
You want to see an even, uniform bead that tracks the joint line without deviation.
Check that the weld ties in smoothly to both sides of the base metal, avoiding sharp shifts or abrupt edges.
After slag removal, the surface should be clean, free from surface-breaking defects like cracks or pits.
Look for the absence of spatter and make certain the weld surface appears continuous and intact.
Although appearance is critical, remember it doesn’t guarantee internal fusion or penetration quality.
You should also confirm that restarts and stop points are neat, with filled craters.
A good stick weld also benefits from the protective slag generated by flux-coated electrodes, which helps reduce oxidation and defects during cooling.
After confirming the weld’s consistency and smooth tie-in, turn your attention to the bead’s shape and profile. A good bead maintains a stable profile throughout the weld, ensuring strength and uniformity.
You want the bead to track the joint line without wandering, with a shape suitable for the joint type. It shouldn’t be too flat or excessively raised. Regular ripples show controlled travel speed and current.
The bead should follow the joint line smoothly, with balanced height and consistent ripples indicating steady technique.
Watch for sudden changes in width or erratic contour, as these indicate technique issues.
Key bead shape and profile qualities include:
Maintaining proper electrode angle and travel speed is crucial to achieving these bead characteristics for a strong, defect-free weld.
While a visually sound weld might look promising, you need to watch for common surface defects that can compromise its integrity.
Porosity appears as small surface pores or bubbles, weakening the weld.
Slag inclusion occurs when you skip proper cleaning between passes, trapping non-metallic particles inside.
Undercut shows as a groove along the base metal beside the bead, reducing cross-sectional strength.
Overlap and cold lap indicate poor fusion where the weld metal doesn’t properly join the base metal, creating weak spots.
Cracking is an immediate red flag and can appear at the toe or within the weld bead.
Inspect your weld after slag removal to detect these defects early.
Avoiding these common surface flaws guarantees your weld maintains both strength and durability.
Proper removal of slag is essential to prevent defects like inclusions and ensure strong weld fusion.
Because the toe and edge shifts form the critical boundary between the weld metal and base material, you need to guarantee they blend smoothly to maintain structural integrity.
The toe and edge shifts are vital boundaries that must blend smoothly to ensure structural integrity.
Sharp or uneven shifts create stress concentrators that can lead to cracks and premature failure.
Smooth toe and edge shifts assure proper fusion, distributing loads evenly and improving fatigue resistance.
When you inspect your weld, focus on these key indicators:
Regular non-destructive inspection helps ensure these critical transitions meet safety and design standards.
Though visual inspection provides essential information about surface conditions, it can’t reveal internal flaws such as incomplete fusion or insufficient penetration.
You’ll detect surface cracks, porosity, undercut, and overlap, but these signs don’t guarantee internal weld integrity.
A good-looking bead with smooth toe changes and consistent profile might still hide subsurface defects that compromise strength.
Visual checks are limited to what the eye can see after slag removal; they won’t show slag inclusions inside the weld or lack of fusion between passes.
To ensure full weld quality, you need supplementary testing methods like ultrasonic or radiographic inspection.
Relying solely on visual inspection risks missing critical defects, so use it as a first step, not the final judgment on stick weld quality.
In addition, proper Non-Destructive Testing techniques are essential to detect internal discontinuities that visual inspection cannot identify.
For mild steel, you’ll want E6011 or E6013 rods. Both offer good penetration and versatility.
For stainless steel, use E308 or E316 rods to resist corrosion.
When welding cast iron, a nickel-based rod like ENi-CI works best.
For aluminum, stick welding isn’t ideal, but if necessary, use a specialized aluminum rod like 4043 with AC current.
Always match the rod to your metal type and welding conditions for best results.
If you crank your welding current way too high, expect a molten lava flood that eats through metal like a hot knife through butter.
Great if you want a crater, not a weld.
Too low, and you’ll get a weak, barely-there bead that’s about as effective as a paper umbrella in a storm.
You’ve got to dial in the current just right to guarantee proper penetration and strong fusion.
This helps avoid defects like undercut or lack of fusion.
To optimize stick welding for thin materials, set your welding current low, usually near the electrode’s minimum amperage, to avoid burn-through.
Use a smaller diameter electrode, like 1/16 inch, for better control. Adjust your arc length short to maintain a stable arc and reduce spatter.
Keep travel speed steady and avoid weaving to minimize heat input. Properly clean the base metal and consider using a welding rod designed for thin sheet applications.
You should replace welding rods whenever they show signs of damage like moisture absorption, rust, or cracking, as these affect weld quality.
Typically, rods exposed to humidity or left out too long need replacing before use.
Also, swap rods if you notice inconsistent arc performance or poor bead appearance during welding.
Regularly inspect rods throughout the job to maintain peak results and avoid defects caused by compromised electrode coatings.
Like putting armor on your weld, post-weld treatments boost durability and corrosion resistance.
You should clean the weld thoroughly to remove slag and spatter.
Applying anti-corrosion coatings like paint or galvanizing protects the metal.
Stress relieving through controlled heating reduces cracking risks.
Also, consider passivation for stainless steel to enhance corrosion resistance.
These steps help your stick weld withstand harsh environments and extend its service life efficiently.
Now that you know what to look for, a consistent bead shape, smooth toe shifts, and the absence of surface defects, can you confidently identify a good stick weld?
Remember, while visual inspection is a vital first step, it has its limits. For critical applications, combining your eyes with testing methods guarantees weld integrity.
Keep these practical pointers in mind to achieve reliable, high-quality stick welds every time you pick up the electrode.