Phone:
(701)814-6992
Physical address:
6296 Donnelly Plaza
Ratkeville, Bahamas.

Phone:
(701)814-6992
Physical address:
6296 Donnelly Plaza
Ratkeville, Bahamas.
The sting of splatter and the frustration of uneven beads make welding a tough skill to start. Beginners often fumble with rods that don’t handle well in tight spots or go through messy slag cleanup. Every botched weld adds to the confusion and slows down progress.
The Forney 30301 E6013 rod eases these struggles with smooth arcs and easy slag removal, perfect for tricky all-position welding. The Hobart 770470 offers broader durability and tensile strength across mild steel projects, focusing on solid penetration. Both rods run well on AC and DC power, catering to different beginner setups.
Hot Max E6013 fills the niche for precise, low-amperage welding on thin metals, creating clean, controlled welds where fine detail counts.
| Image | Name | Editor's Rating | Price |
|---|---|---|---|
|
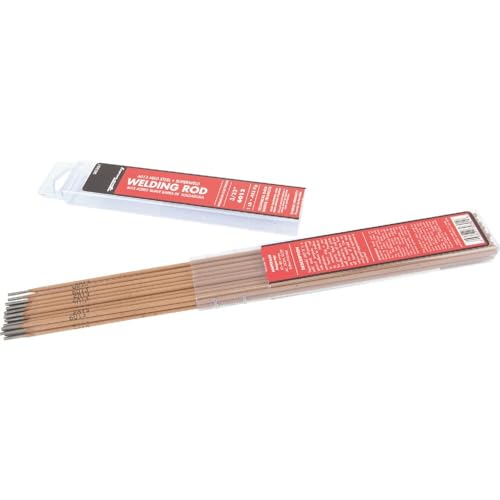
Forney 30301 E6013 Welding Rod, 3/32-Inch, 1-Pound
|
|
|
|
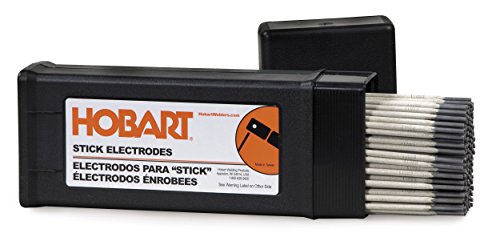
Hobart 770470 6013 Stick, 1/8-10 lb. | Light-to-medium penet...
|
|
|

|
Hot Max 22075 1/16-Inch E6013 1# ARC Welding Electrodes
|
|
|

|
YESWELDER E6013 3/32'' 5LB Welding Rods Stick Electrodes
|
|
|
|
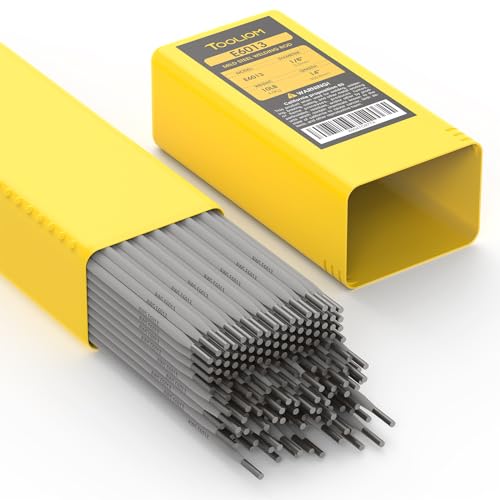
TOOLIOM E6013 Welding Rod Carbon Steel Stick Electrodes, 1/8...
|
|
Choosing the right welding rod sets the foundation for successful projects. These carefully selected rods combine ease of use, versatility, and reliability, helping newcomers build confidence with each weld.
Tackling difficult welds in awkward positions becomes simpler with this tool, designed for all-position welding. It works well even in tight fits or shallow penetration scenarios, making complex setups less intimidating.
Offering a smooth and consistent arc, it runs perfectly on both AC and DC power sources, delivering excellent wetting action for neat, flat beads. You’ll appreciate the reduced splatter and ease of cleaning slag, which saves time on post-weld finishing.
Each rod is crafted for mild steel projects requiring low spatter and precise control—ideal for vertical down welding where steady performance counts. Forney’s engineering ensures steady results even when conditions aren’t perfect.
Its moderate thickness of 3/32-inch balances accessibility and durability, supporting up to 80 amps of power. The rods offer a tensile strength around 60,000, sufficient for many general fabrication needs.
Whether you’re repairing, fabricating, or learning weld fundamentals, Forney’s rod stands out as a reliable ally.
Best for: Hobbyists and craftsmen seeking a practical solution for versatile mild steel welding tasks.
Pros:
Cons:
Light to medium penetrating capabilities make these electrodes a solid choice for various welding tasks. Their carbon steel composition supports a tensile strength reaching 60,000 PSI, offering dependable weld integrity when working on mild steel projects.
Compatible with AC, DCEP (reverse polarity), and DCEN (straight polarity) power sources, these rods provide versatile usage options in different welding environments. The adaptability allows handling of several welding machines without needing specialized electrodes for each.
Hobart’s design packs these rods in a sturdy case, helping maintain their condition and ensuring ease of storage. The 1/8-inch diameter and 10-pound quantity balance usability and supply for extended welding sessions.
A consistent arc performance helps beginners develop control during the welding process without being overwhelmed by unpredictable behavior. This reliability aids in gaining practical skills more efficiently.
Best for: Hobbyists and newcomers needing versatile, stable electrodes for foundational stick welding practice and small- to medium-scale projects.
Pros:
Cons:
Working with thin materials or tackling light repair jobs calls for a welding rod that offers easy strike and smooth arc stability. Hot Max delivers a 1/16-inch electrode tailored to provide consistent performance between 20-40 amps, making it ideal for controlled, precise welds. The rod is engineered to help maintain a clean, stable arc, which reduces spatter and simplifies bead formation.
Designed as a hand-powered arc welding consumable, its slim diameter offers excellent maneuverability in tight spots or when welding delicate metals. Paired with a moderate amperage range, it allows for fine control—especially valuable when learning proper technique or working on thin gauge metals.
Hot Max’s electrode features a flux coating that supports easy slag removal and producing strong welds without excessive cleanup. Its dimensions and weight suit portability and long welding sessions without hand fatigue. Whether focused on maintenance tasks or small fabrication projects, this rod facilitates a balanced, manageable welding experience.
The electrode provides a respectable balance between ease of use and quality output, suitable for various mild steel applications. It’s a dependable choice that helps you build confidence in your welds without overwhelming complexity. Durability combined with steady arc characteristics make Hot Max a practical tool for those becoming familiar with arc welding basics.
Best for: Hobbyists and entry-level welders working on light to medium gauges who seek dependable arc start and smooth welds.
Pros:
Cons:
Mastering metal joining requires clarity and control. Designed to adapt, these rods deliver all-position welding versatility, making even tricky angles manageable for emerging welders.
Their mild-steel core suits light gauge and sheet metal without demanding complex setups.
Operating seamlessly on both AC and DC currents, the rods thrive under low-voltage AC machines, providing stable arcs that help you focus on technique rather than gear complications. Low spatter and excellent slag removal mean less cleanup and sharper, neater welds, which can boost both confidence and project quality.
Built specifically for general use, these electrodes shine where tight fits or shallow penetration are needed, adapting to less-than-ideal joint conditions while maintaining consistent performance. The virtually self-cleaning vertical down fillet application simplifies vertical welding tasks, a real benefit for beginners wrestling with gravity.
With a size that balances control and coverage, each 3/32″ rod supports amperage from 45 to 90, providing a forgiving range conducive to learning. YESWELDER brings reliability to your practice sessions with these steady and approachable sticks.
Best for: Novices seeking a manageable, versatile option for mild steel projects and initial welding practice.
Pros:
Cons:
Struggling with welding thin metal plates or handling projects with tricky joint fits? This batch of TOOLIOM E6013 carbon steel rods is built for versatility across numerous mild steel applications. With a 1/8 inch diameter and a 10-pound weight, these rods make intermittent welding of sheets or pipelines much more manageable.
Enjoy the soft, stable arc that produces minimal spatter and smoke, which will help you maintain cleaner welds and less cleanup. The rods work on both AC and DC power sources, granting you freedom to choose your equipment setup without compromise.
Weld in any position—from vertical down to horizontal—with rods that nearly self-clean as they work, making arc restarts straightforward and less frustrating. This all-position welding convenience supports smoother surfaces, even when covering or repairing less-than-perfect fits.
Designed for medium to shallow depth welding, these electrodes from TOOLIOM strike a balance between control and efficiency, perfect for beginners who want a dependable, forgiving rod. Operating within a 70 to 120 amp range, they adapt well to a variety of skill levels and metal conditions.
Best for: Hobbyists and novice welders undertaking thin metal fabrication and maintenance, especially in projects requiring neat, clean finishes without complex setups.
Pros:
Cons:
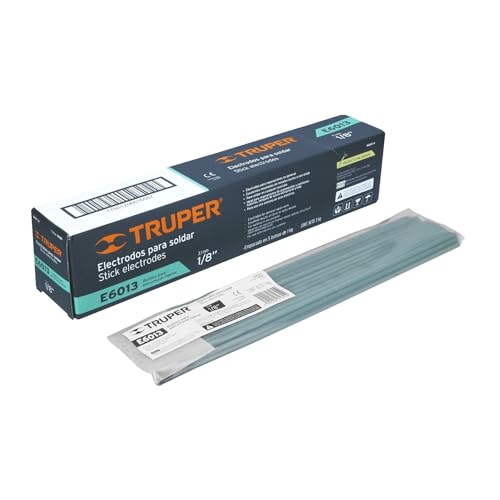
Welding projects often challenge newcomers to find a rod that balances ease of use and dependable performance. The Truper E6013-4 electrode offers a smooth arc with minimal spatter, making it easier to manage during the learning curve of stick welding. Its moderate penetration suits thinner metals, reducing the risk of burn-through often encountered by beginners.
Designed for versatility, this electrode performs well with AC or DC power sources, expanding your setup options without added complexity. The E6013 coating enhances powdery slag control, which peels away more cleanly than some alternatives, helping maintain a cleaner workspace with less rework.
Weighing just over two pounds, it’s lightweight enough for easy handling during extended practice sessions, encouraging better control and weld quality from the outset. Truper’s quality manufacturing ensures consistent electrode diameter and composition, which means fewer surprises when striking arcs.
Recognized for its balance between penetration depth and bead appearance, this rod also absorbs variations in technique, forgiving the common mistakes beginners make. Using it regularly will build your confidence around different joint configurations and lead to better weld bead consistency quickly.
Best for: Hobbyists and novices experimenting with mild steel who need a reliable electrode that adapts to varying skill levels and equipment setups.
Pros:
Cons:
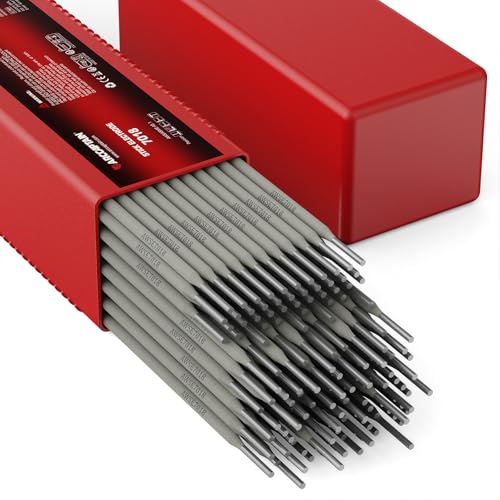
Handling various welding positions can be intimidating, yet the right electrode can simplify this challenge drastically. Designed with a low hydrogen core, these rods minimize cracking risks and maintain weld integrity under stress. The E7018 electrode is renowned for its high tensile strength and consistent, smooth arc, enabling precise, professional welds with minimal spatter.
Engineered for versatility, it works on both AC and DC reverse polarity, making it adaptable to different welding setups you might encounter. Welding steel of varying carbon levels—from structural frames to pipelines—is within reach thanks to the rod’s broad compatibility.
ARCCAPTAIN ensures each rod delivers a stable arc performance highlighted by excellent x-ray quality welds, critical for demanding structural applications. Weighing 10 pounds and sized at 1/8 inch diameter, these electrodes provide a substantial supply for ongoing projects without frequent replacements.
Choosing an electrode with fewer defects means your work benefits from smoother application and robust welds, even if you’re still refining your technique. Less spatter also means less cleanup, helping you focus on honing your skills rather than managing mess.
Best for: Those preparing to tackle low to high carbon steel joints in varied positions, including hobbyists and trainees seeking reliable, strong welds across multiple materials.
Pros:
Cons:

Handling thin steel plates becomes much more manageable with this welding rod built for precision and control. Its titanium oxide coating ensures a stable arc with minimal spatter, making your weld seams cleaner and easier to manage during fine operations.
Maintaining arc stability is key, and this electrode stands out by offering a smooth burn and effortless re-ignition, ideal for delicate work and improving molten pool control. This attribute helps reduce welding fatigue by providing consistent performance.
Versatility shines through with the capability to weld in all positions—horizontal, vertical, overhead, and more. Its adaptability makes it a practical choice when working within narrow spaces or on complex structural projects where maneuverability is limited.
Typically favored for its effectiveness on steel and thin metal sheets, this Sunstac rod excels in producing neat, high-quality surface welds, especially where cover welding is required. Its ability to maintain a steady arc enhances the overall finish of your projects.
Best for: Hobbyists and new welders tackling thin steel and complex welds who need dependable arc stability and minimal cleanup.
Pros:
Cons:
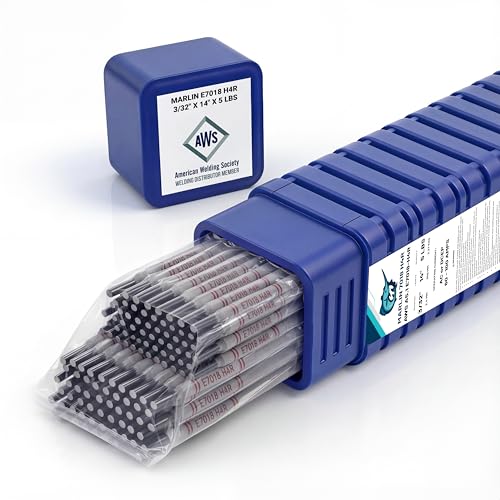
Achieving consistent, strong welds requires electrodes that handle every position with ease. These rods are designed for versatility, working smoothly in flat, vertical, overhead, and horizontal orientations, whether you’re on the job site or in the workshop.
Engineered to deliver around 70,000 to 84,000 psi tensile strength, Metal Marlin’s offering ensures joints that stand up to tough conditions. The low-hydrogen content reduces the chance of cracking, contributing to durable, code-quality welds.
Expect a stable arc and minimal spatter, which translates to less time spent on cleaning.
Vacuum-sealed packaging protects the rods from moisture, maintaining their low-hydrogen quality. This feature is crucial to avoid pre-baking and helps maintain the electrodes’ performance on arrival.
Designed to meet the standards set by AWS and ASME, these electrodes suit a wide range of welding tasks—from structural steel and fabrication to heavy equipment and piping systems.
Metal Marlin provides a reliable solution that supports both AC and DC welding machines, broadening its usability.
Best for: Craftsmen and hobbyists needing dependable all-position electrodes with consistent strength and ease of use.
Pros:
Cons:
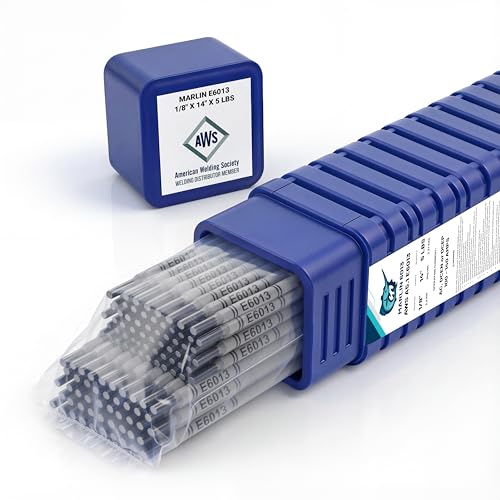
Navigating the world of welding rods can initially feel overwhelming, especially when managing thin metals and sheet materials. The METAL MARLIN E6013 rods create a calm, stable arc that simplifies welding thin gauge steel, ductwork, and brackets. Their forgiving nature helps protect delicate workpieces while delivering clean, smooth welds.
Designed to perform effortlessly in all positions—flat, horizontal, vertical, or overhead—these electrodes give you reliable control over heat penetration. That makes consistent, professional-grade results within reach even when you’re still mastering the basics.
Experience easy slag removal and significantly less cleanup due to the low-spatter arc, which speeds up workflow and reduces frustration on repairs. Plus, their compatibility with both AC and DC power sources, including low-voltage 110V machines, broadens your setup options.
With a tensile strength around 60,000 psi, the rods deliver strong, durable joins suited for automotive, farm, and light fabrication projects. The meticulous design focuses on offering smooth, forgiving welds that encourage skill development without punishing errors harshly.
Best for: Hobbyists and newcomers requiring user-friendly equipment to weld sheet metal and mild steel confidently across multiple positions.
Pros:
Cons:
| Product Name | Rod Diameter | Amperage Range | Material | Weight |
|---|---|---|---|---|
| Forney 6013 Mild Steel Rod | 3/32-Inch | Up to 80 A | Mild Steel | 1 pound |
| Hobart 6013 Carbon Steel | 1/8-Inch | Not Specified | Carbon Steel | 10 pounds |
| Hot Max 6013 Small Diameter | 1/16-Inch | 20–40 A | Not Specified | 1 pound |
| YESWELDER E6013 Multi-Use | 3/32-Inch | 45–90 A | E6013 Mild Steel | 5 pounds |
| TOOLIOM E6013 General Rod | 1/8-Inch | 70–120 A | E6013 Low Carbon Steel | 10 pounds |
| TRUPER E6013 1/8″ Rod | 1/8-Inch | Not Specified | Not Specified | 2.2 pounds |
| ARCCAPTAIN E7018 Low Hydrogen | 1/8-Inch | Not Specified | E7018 Low Hydrogen Steel | 10 pounds |
| Sunstac E6013 Titanium Coated | 1/8-Inch | Not Specified | E6013 Steel | 5 pounds |
Getting the right welding rod can turn a frustrating learning curve into an enjoyable, rewarding experience. Focusing on key factors will help you match your rod to your project, skill level, and equipment – so you can weld confidently from the start.
Rod diameter influences the type of metal thickness it can effectively weld, serving as a critical measure of compatibility. A thicker rod typically handles heavy-gauge metals, while thinner rods excel in light-gauge or delicate applications. For example, a 1/16-inch rod like Hot Max’s E6013 is designed for thin materials, providing steady control between 20 to 40 amps. Conversely, a 1/8-inch rod such as TOOLIOM’s E6013 suits heavier metal sections and higher current ranges up to 120 amps.
Diameter affects heat input and penetration depth; thinner rods deliver less heat, minimizing burn-through risk on thin sheets. Meanwhile, larger diameters create broader weld beads and stronger joints but require more skill. Matching rod diameter precisely to your metal gauge prevents defects like weak welds or excessive spatter.
Ignoring rod diameter leads to either insufficient fusion or over-penetration mistakes, causing fragile welds or damage. Beginners who pick the wrong thickness may waste materials, struggle with arc control, or develop poor bead appearance, hampering progress early on.
The core material inside the welding rod shapes its mechanical strength and arc behavior, making it a make-or-break feature in beginner-friendly electrodes. Common cores include mild steel and low hydrogen steel. Mild steel cores, like Forney 30301’s, provide balance and versatility for general mild steel fabrication, while low hydrogen cores, such as ARCCAPTAIN’s E7018, minimize hydrogen-induced cracking risks during critical welds.
Core composition directly relates to tensile strength and welding position flexibility. For instance, Hobart’s carbon steel electrodes offer strong welds rated around 60,000 PSI, suitable for structural work. Low hydrogen rods produce cleaner deposits with less porosity, but often demand tighter storage and drying control. Coatings like titanium oxide found in Sunstac’s rods improve arc stability and reduce spatter by influencing slag formation and molten droplet behavior.
Choosing rods with unsuitable core types results in welds that can crack, lack strength, or produce excessive slag. For new welders, incompatible materials complicate technique development and may lead to costly redo work or safety concerns.
Welding rod adaptability to different positions—flat, vertical, overhead, or horizontal—significantly affects comfort and quality for beginners. Electrodes labeled as “all-position,” like YESWELDER E6013 and TOOLIOM rods, allow welders to work confidently in diverse setups without switching rods or struggling with gravity-driven weld issues.
Position versatility arises from flux coating chemistry and rod rigidity, influencing how molten metal behaves during the weld. A well-formulated coating controls melting speed and slag coverage, supporting stable arcs when welding upside down or on vertical joints. The flux layer helps contain weld puddles, reduce dripping, and suppress spatter, which beginners find easier to manage.
Using rods limited to flat or horizontal applications restricts practice and can produce poor weld consistency on complex joints. New welders may face frustration when rods crack or drip excessively in challenging positions, hindering technique confidence.
The amperage rating of a welding rod defines the optimal current range for establishing a stable arc and effective penetration, a vital practical consideration for beginners tuning their machines. For example, YESWELDER’s rods operate efficiently from 45 to 90 amps, while Hot Max’s 1/16-inch model thrives within a narrower 20 to 40 amps window, ideal for delicate control.
Compatibility with different power sources such as AC, DC reverse polarity (DCEP), or DC straight polarity (DCEN) enhances flexibility. Many beginner rods like Forney 30301 and TRUPER E6013 function well on both AC and DC currents, simplifying equipment selection. The electrical characteristics of the rod’s coating determine arc initiation ease and stability at varying currents. For instance, titanium oxide coatings enhance re-ignition capabilities under fluctuating amperages.
Ignoring amperage ranges causes unstable arcs, excessive spatter, or poor penetration. A new welder using a rod outside its current rating may struggle with arc starting or burn-through, which leads to wasted rods, frustration, and slow skills development.
Arc stability and minimal spatter production impact weld quality and cleanup time, crucial for those still refining hand control. Rods known for smooth arcs, like Truper E6013-4 and Forney 30301, reduce erratic arc wandering and produce cleaner bead profiles. This feeds back into better learning by providing immediate visual feedback on travel speed and electrode angle.
Smooth arcs arise from uniform flux coatings that encourage even melting and stable electrical conductivity. Lower spatter results from chemical additives that regulate molten droplet transfer to the base metal. These characteristics prevent slag blowoff and promote consistent bead wetting. For instance, rods coated with rutile compounds improve arc smoothness and bead appearance.
Neglecting arc quality means dealing with excessive sparks and uneven welds that complicate post-welding cleanup. Beginners facing uncontrolled arcs often get discouraged due to messy, inconsistent results, slowing skill progression and adding frustration.
The slag that forms on top of the weld bead insulates the molten metal and protects it as it cools; how easily this slag peels off directly affects finishing time and the overall look of the weld. Rods like Forney 30301 and YESWELDER E6013 are praised for producing easily removable slag that leaves neat beads behind. This characteristic is a small but meaningful convenience for beginners.
Flux composition and coating thickness govern slag hardness and adherence. A well-balanced coating melts to form slag that solidifies into a brittle layer, which can be chipped away without damaging the bead. Excessively thick or contaminated coatings create hard-to-remove slag, increasing cleanup duration and risk of bead distortion.
Overlooking slag removability leads to additional grinding or chiseling effort, increasing fatigue and risking weld damage. New welders may find sticky slag discouraging, especially when initial weld appearances are critical for motivation.
Welding rods like the Forney 30301 E6013 stand out due to their smooth, consistent arc and all-position usage, which helps newcomers tackle different welding angles with confidence. Their ability to run on both AC and DC power makes setup simpler, removing equipment compatibility worries.
This rod also offers low spatter and easy slag removal, reducing tedious post-weld cleanup—an important consideration for beginners still mastering techniques. Its 3/32-inch diameter balances manageability and weld strength.
Focus on rods designed for mild steel with forgiving arc characteristics to ease your initial skill development and avoid burn-through on thin materials.
The diameter influences current settings and weld penetration; smaller rods like the Hot Max 1/16-inch E6013 are ideal for thin materials and light repair work, offering precise control at 20-40 amps. In contrast, thicker rods such as the 1/8-inch TOOLIOM E6013 handle heavier gauge steel and higher amperage applications.
Choosing rod size should align with your project’s material thickness and the welding machine’s amperage capacity. Overly thick rods on thin metal risk burn-through, while thin rods may lack penetration on thicker stock.
Match your rod diameter with your power source settings and metal thickness for cleaner, stronger welds and to build technique efficiently.
E6013 rods are widely recommended for beginners because they provide a stable arc, low spatter, and adaptability for all-position welding. Their light to moderate penetration is forgiving and helps novices avoid common pitfalls like excessive burn-through or difficult slag removal.
For example, the YESWELDER E6013 rods perform well on AC or DC machines and excel on thinner gauge metals, simplifying the learning curve. Their mild-steel core and flux coating contribute to consistent bead quality and easier slag cleanup.
Sticking with E6013 rods until you get comfortable will improve your confidence before moving on to more specialized electrodes or complex materials.
Low hydrogen rods such as the ARCCAPTAIN E7018 reduce the risk of weld cracking and improve joint durability by releasing minimal hydrogen during welding. Although generally preferred for structural or high-stress work, they provide a smooth arc and strong welds that benefit beginners aiming for professional results.
However, E7018 rods typically require controlled storage to remain dry and perform well, which might add complexity for novices. Still, their high tensile strength and weld integrity make them worth considering as skills advance.
If opting for low hydrogen rods early on, store them properly to prevent moisture absorption, which can cause weld defects and frustration during use.
Versatile rods like the Hobart 1/8-inch carbon steel electrodes work across various mild steel tasks due to their compatibility with multiple polarity types (AC, DCEP, DCEN) and moderate penetration. Using a rod that suits most common welding scenarios helps beginners avoid juggling numerous types prematurely.
Yet, distinct projects might demand specific features—for example, thinner metals benefit from smaller diameter rods like the Hot Max 1/16-inch, while heavier repairs need larger, stronger rods. Understanding project requirements aids in selecting the right electrode for efficiency and quality.
Keep one reliable all-position rod handy for general use, but expand your collection gradually as you encounter specialized welding needs.
Choosing the right welding rod transforms your initial welding journey by offering better control and fewer errors. This change helps beginners progress faster with improved weld quality and less frustration.
For thin metals, smaller rods like 3/32-inch E6013 are ideal for maneuverability and versatility, while thicker steels benefit from 1/8-inch rods that provide deeper penetration. Delicate projects call for finer rods such as 1/16-inch sizes for precise handling.
Starting with a suitable rod size at the correct amperage is essential to prevent defects. Also, watch for moisture in rods, as it can cause cracks. Consistently using the right rod improves welding consistency and builds confidence with practice.
Last update on 2026-10-13 / Affiliate links / Images from Amazon Product Advertising API